验收快报丨国内知名大型机床厂“Thermal CMS热误差补偿系统”项目验收
近日,西格数据为处于中国·四川的知名大型机床厂部署了“Thermal CMS热误差补偿系统”项目,并顺利通过客户验收!首先非常感谢客户信任和项目团队的辛勤付出,使得客户端能够快速应用机床热误差补偿,该项目的核心目标是通过实时监测机床温度变化,精确计算并补偿热变形对加工精度的影响,确保在温度变化条件下机床保持高稳定性,从而提高工件加工的精度和一致性。
1、客户背景介绍
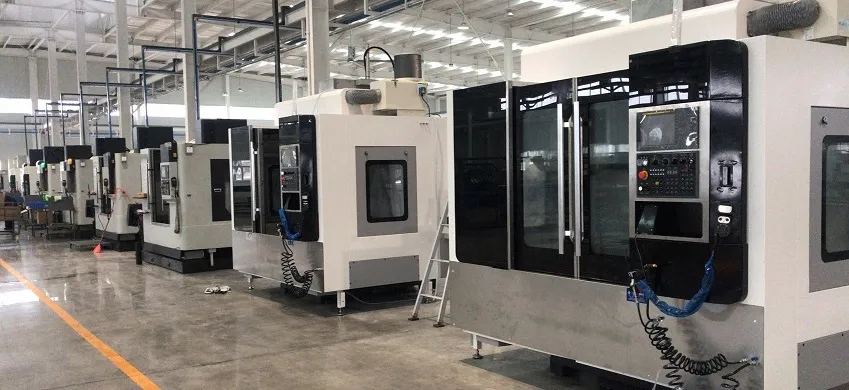
该客户是一家专业从事数控机床、非标设备、自动化设备等专用设备制造业为主的企业,公司秉承科技创新的理念,拥有一支经验丰富的研发团队,已成功研发并掌握了21项核心自主知识产权,先后通过ISO9001质量管理体系认证、ISO14001环境管理体系认证,以及武器装备质量管理体系认证,公司产品以性能稳定、精度高、可靠性好等特点,广泛应用于航空航天、汽车制造、模具加工等多个领域,深受广大用户的信赖与好评。

客户痛点和需求:
1)加工精度受热误差影响,导致产品质量不稳定,实时补偿确保工件高精度加工;
2)热误差导致机床加工效率下降,增加生产周期,实时补偿提升机床运行效率;
3)热误差引起的材料浪费和返工增加生产成本,减少因热误差造成的废品率,降低成本;
4)传统校准方法难达高精度的加工要求,智能化的热误差补偿系统,满足精密加工高标准;
2、项目部署
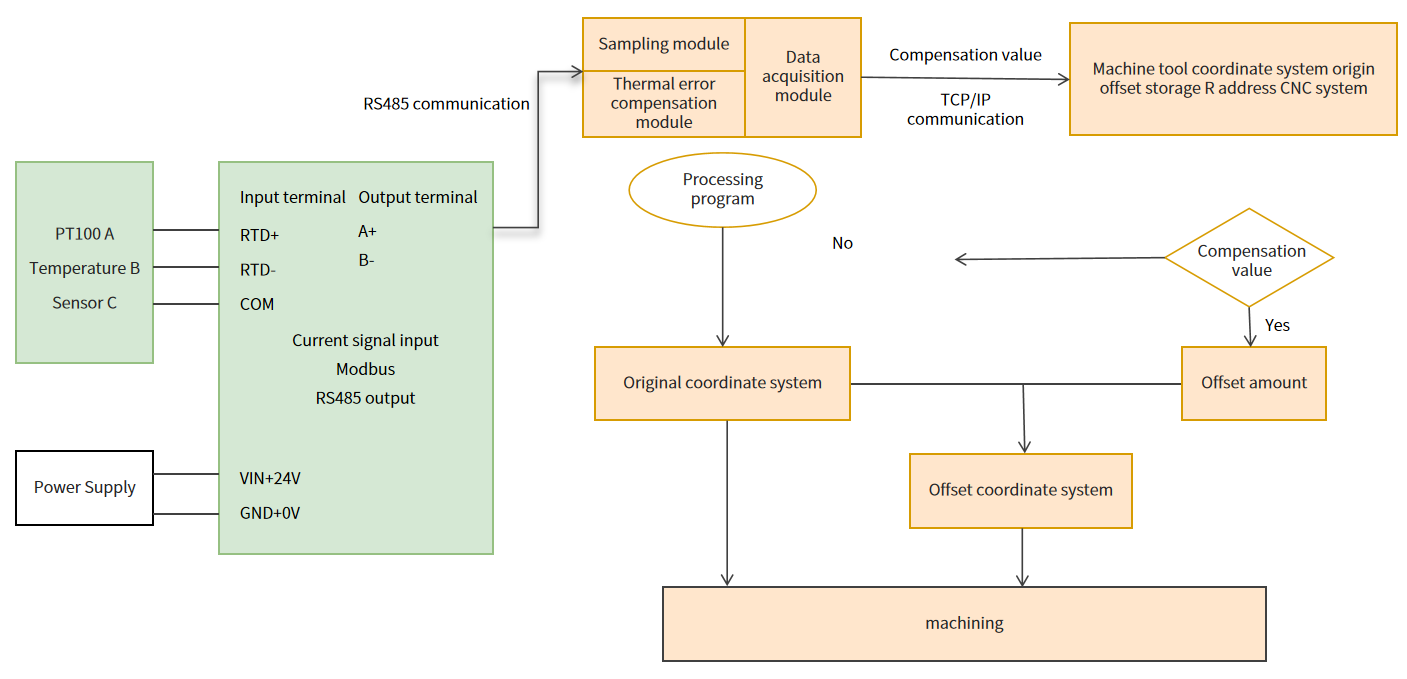
热误差补偿系统-补偿原理图
热误差补偿系统(Thermal Compensation Management System,Thermal CMS)是一种用于提高机床加工精度的技术解决方案。它通过监测和分析机床在运行过程中由于温度变化引起的误差,并采取措施对这些误差进行补偿,确保机床在温度变化的环境下仍能保持高精度的加工性能,这一技术对于航空航天、精密模具等行业的精密加工至关重要。

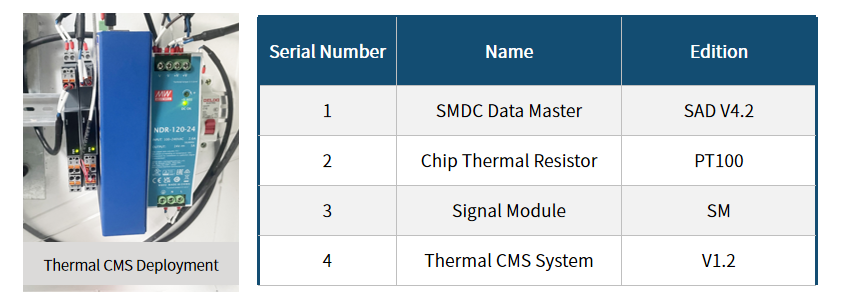
2.2 热误差补偿系统-软硬件配置

3、项目应用实施成果
3.1 X轴热伸长量和温度变化测试对比结果

未开启热补偿前:X轴热伸长量变化175μm,主轴电机温度变化11.7℃
开启热补偿后:X轴热伸长量变化50μm,主轴电机温度变化10.9℃
应用效果:热伸长量减少了125μm,热补偿效果能达到71.42%
3.2 Y轴热伸长量和温度变化测试对比结果

未开启热补偿前:Y轴热伸长量变化144μm,主轴电机温度变化6.1℃
开启热补偿后:Y轴热伸长量变化32μm,主轴电机温度变化5.2℃
应用效果:热伸长量减少了112μm,热补偿效果能达到77.78%
3.3 Z轴热伸长量和温度变化测试对比结果

未开启热补偿前:Z轴热伸长量变化53μm,主轴电机温度变化3.5℃
开启热补偿后:Z轴热伸长量变化12μm,主轴电机温度变化2.2℃
应用效果:热伸长量减少了41μm,热补偿效果能达到77.36%
3.4 项目验收报告:
通过SIGER项目团队和客户项目的紧密配合,西格数据团队成功实现热误差补偿系统的部署,项目顺利通过客户验收,产品应用效果得到了客户的高度认可,期待下一次进一步为客户提供服务。

4、快速了解SIGER Thermal CMS 热误差补偿管理系统
西格数据热误差补偿系统(Thermal Compensation Management System,Thermal CMS),通过测量和补偿系统减少数控机床在加工过程中由于温度变化引起的热误差,从而提高加工精度和稳定性;基于机床嵌入式结构,结合热误差补偿模型,实时输出补偿值,有效提高产品加工精度,降低产品报废率。
西格数据 热误差补偿系统适配范围:
■ 适用机床类型:数控车床、车铣复合等多种机床切削场景;
■ 适用加工工艺:大批量重复加工、大批量嵌套工艺加工、小批量加工、长时间模具加工、粗/精加工等多种工艺类型(背吃刀量不低于10丝);
■ 适用加工方式:车削加工|铣削加工|齿面加工|曲面等
如您对西格数据的产品感兴趣,可以拨打电话:189 6235 3927(微信同号),也可以留下您的需求、电话和公司名称,我们会第一时间与您联系。
>>点击查看SIGER热误差补偿管理系统<<
Recently, SIGER Data deployed a "thermal error compensation system" project for a well-known large machine tool factory in Sichuan, China, and successfully passed the customer's acceptance! First of all, I would like to thank the customer for their trust and the hard work of the project team, which enabled the client to quickly apply machine tool thermal error compensation. The core goal of this project is to monitor the temperature changes of the machine tool in real time, accurately calculate and compensate for the impact of thermal deformation on machining accuracy, and ensure that the machine tool maintains high stability under temperature changes, thereby improving the accuracy and consistency of workpiece processing.
1. Customer background introduction:
The customer is an enterprise specializing in the manufacturing of special equipment such as CNC machine tools, non-standard equipment, and automation equipment. The company adheres to the concept of scientific and technological innovation and has an experienced R&D team. It has successfully developed and mastered 21 core independent intellectual property rights, and has passed ISO9001 quality management system certification, ISO14001 environmental management system certification, and weapons and equipment quality management system certification. The company's products are characterized by stable performance, high precision, and good reliability. They are widely used in aerospace, automobile manufacturing, mold processing and other fields, and are deeply trusted and praised by users.
Customer pain points and needs:
1) Processing accuracy is affected by thermal errors, resulting in unstable product quality. Real-time compensation ensures high-precision processing of workpieces.
2) Thermal errors cause machine tool processing efficiency to decrease, increasing production cycles. Real-time compensation improves machine tool operation efficiency.
3) Material waste and rework caused by thermal errors increase production costs. Reducing the scrap rate caused by thermal errors reduces costs.
4) Traditional calibration methods are difficult to achieve high-precision processing requirements. Intelligent thermal error compensation systems meet high standards for precision processing.
2. Project deployment
2.1 Thermal Compensation Management System - Compensation Principle Diagram
Thermal Compensation Management System (Thermal CMS) is a technical solution for improving the machining accuracy of machine tools. It monitors and analyzes the errors caused by temperature changes during the operation of the machine tool, and takes measures to compensate for these errors, ensuring that the machine tool can still maintain high-precision machining performance in an environment with temperature changes. This technology is crucial for precision machining in industries such as aerospace and precision molds.
2.2 Thermal Compensation Management System - Software and Hardware Configuration
3. Project application implementation results
3.1 Comparison results of X-axis thermal elongation and temperature change test
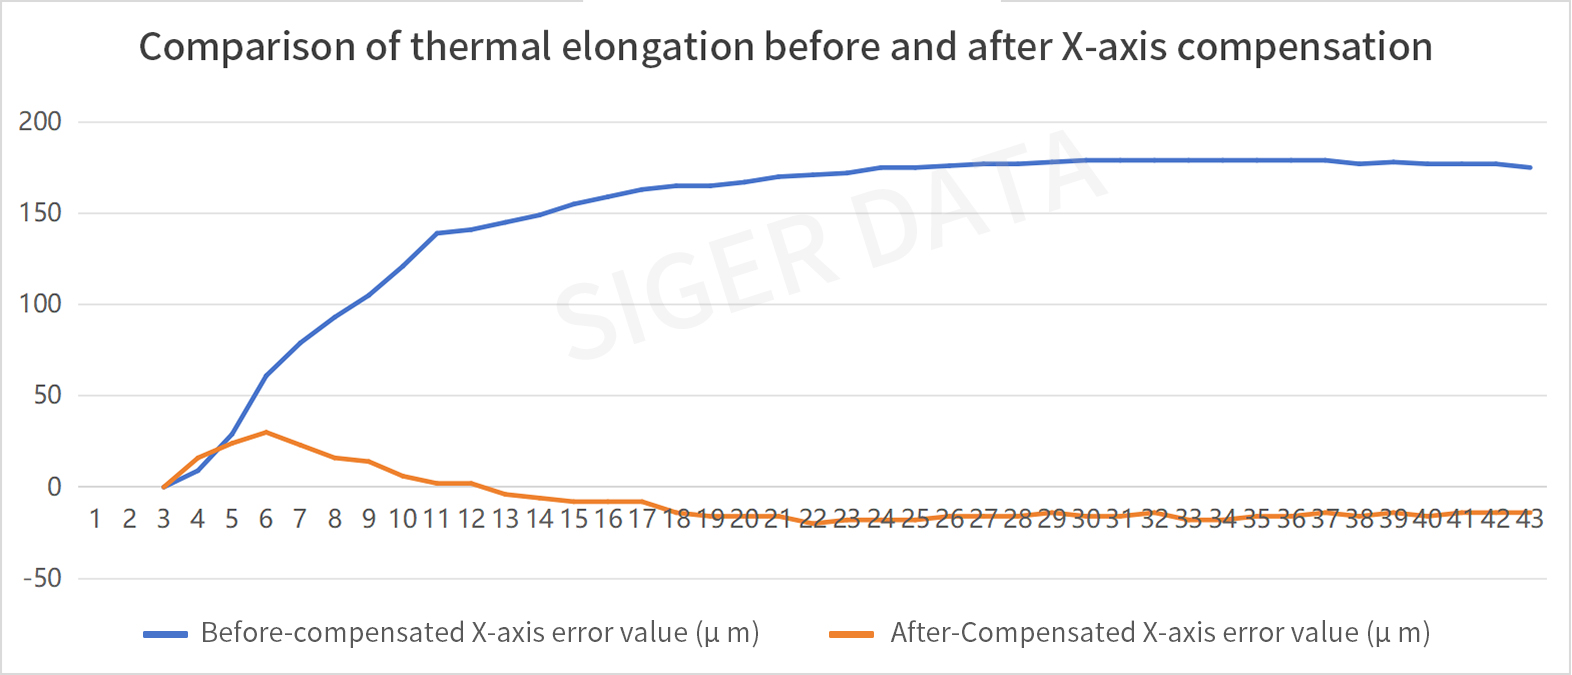
Before thermal compensation is turned on: X-axis thermal elongation changes by 175μm, spindle motor temperature changes by 11.7℃.
After thermal compensation is turned on: X-axis thermal elongation changes by 50μm, spindle motor temperature changes by 10.9℃.
Application effect: thermal elongation is reduced by 125μm, and the thermal compensation effect can reach 71.42%.
3.2 Comparison results of Y-axis thermal elongation and temperature change test
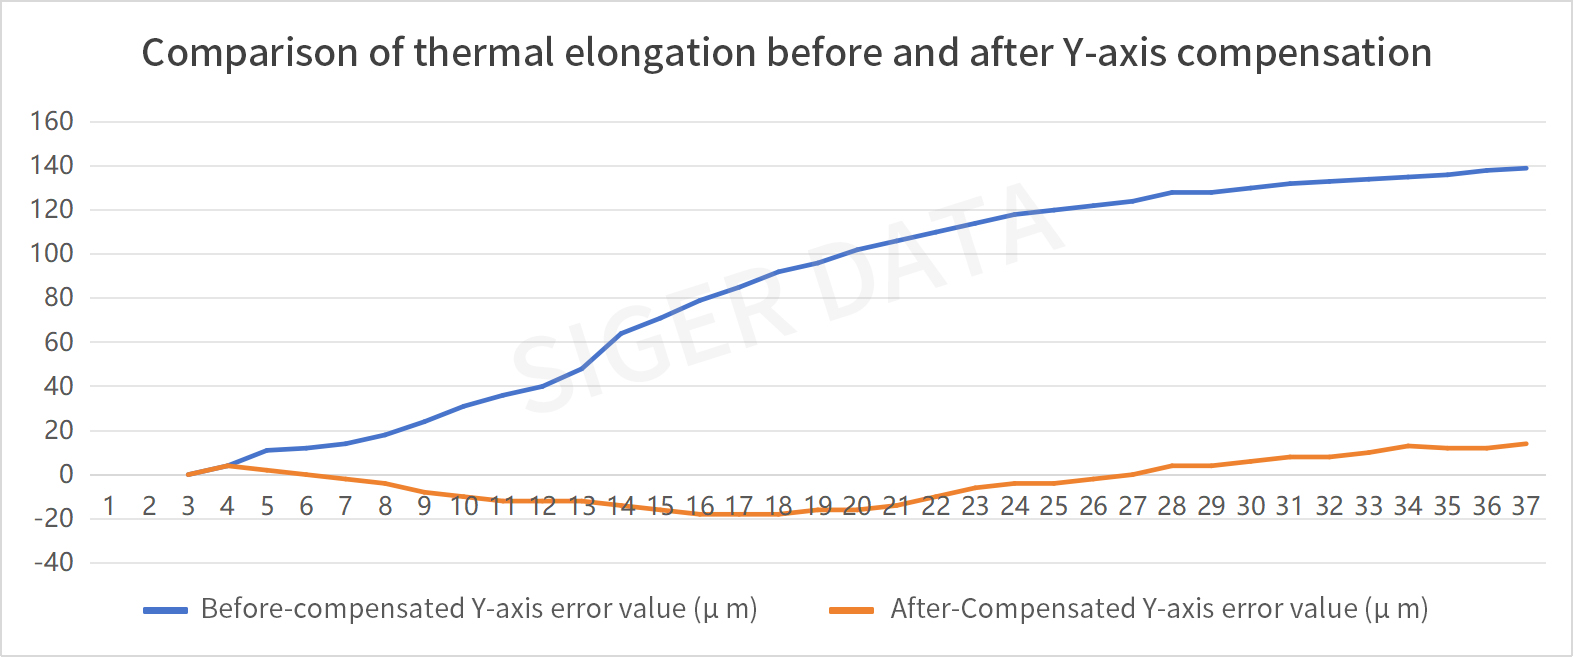
Before thermal compensation is turned on: Y-axis thermal elongation changes by 144μm, and spindle motor temperature changes by 6.1℃.
After thermal compensation is turned on: Y-axis thermal elongation changes by 32μm, and spindle motor temperature changes by 5.2℃.
Application effect: Thermal elongation is reduced by 112μm, and the thermal compensation effect can reach 77.78%.
3.3 Comparison results of Z-axis thermal elongation and temperature change test
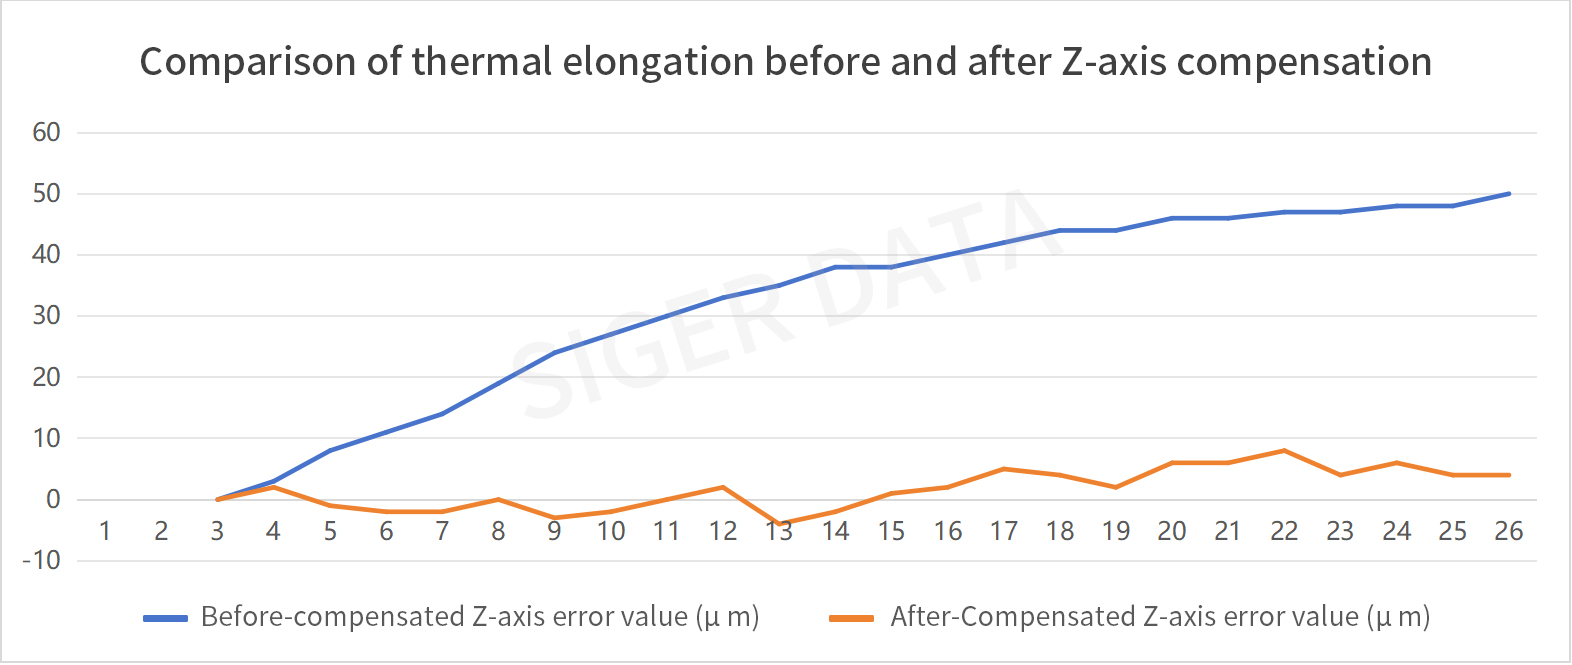
Before thermal compensation is turned on: Z-axis thermal elongation changes by 53μm, spindle motor temperature changes by 3.5℃.
After thermal compensation is turned on: Z-axis thermal elongation changes by 12μm, spindle motor temperature changes by 2.2℃.
Application effect: Thermal elongation is reduced by 41μm, and the thermal compensation effect can reach 77.36%.
Scope of adaptation of SIGER Thermal Compensation Management
■ Applicable machine tool types: CNC lathes, turning and milling compound and other machine tool cutting scenarios.
■ Applicable processing technology: large-scale repeated processing, large-scale nested process processing, small-scale processing, long-term mold processing, rough/finishing processing and other process types (back cutting amount is not less than 10 wires).
■ Applicable processing methods: turning processing | milling processing | tooth surface processing | curved surface, etc.
If you are interested in SIGER products, you can contact us by phone or email, or submit your requirements by leaving a message, and we will arrange personnel to contact you as soon as possible.
--------------------------------------------------------------------------------------------------------------------------------------------------------
Official Contact Info:
Email: marketing@siger-data.com
WhatsApp:+86 189 6235 3927
WeChat:189 6235 3927

